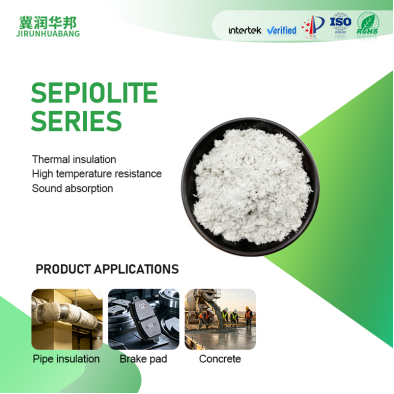
Under the global trend of industrial asbestos-free environmental upgrading and new material iteration, sepiolite fiber has become an indispensable core functional mineral raw material in various industries, including friction materials, refractory building materials, fine chemicals, petroleum drilling, and environmental governance. As a natural hydrated magnesium silicate clay mineral fiber, standard α-type high-purity sepiolite fiber is processed from high-quality raw sepiolite ore through precise screening, multi-stage purification, high-pressure defibering, high-temperature activation, graded modification and other sophisticated processes. It completely eliminates the safety hazards of traditional asbestos fibers and is internationally recognized as a high-performance, pollution-free, and highly adaptable alternative to asbestos.
In terms of microscopic crystal structure and physical properties, sepiolite fiber features a unique needle-like tubular crystal structure with slender and flexible single fibers and excellent length-diameter ratio. Its interior is filled with three-dimensional connected tunnel micropores with uniform and dense pore distribution, endowing it with comprehensive properties far superior to ordinary kaolin, talc powder and bentonite. It has a specific surface area of 200–900 m²/g and high porosity, delivering powerful physical adsorption, ion exchange and locking capabilities. It can stably absorb 2-3 times its own weight of water, and efficiently capture and assist in degrading heavy metal ions, volatile organic compounds, oil impurities, odor molecules and pigment particles in industrial systems. Different from traditional mineral fillers, sepiolite fiber is non-toxic, odorless, free from carcinogenic dust risks, and contains no harmful components such as asbestos and quartz sand. It fully complies with EU REACH, ROHS, US EPA and domestic environmental standards, enabling smooth exports to global markets without environmental compliance barriers.
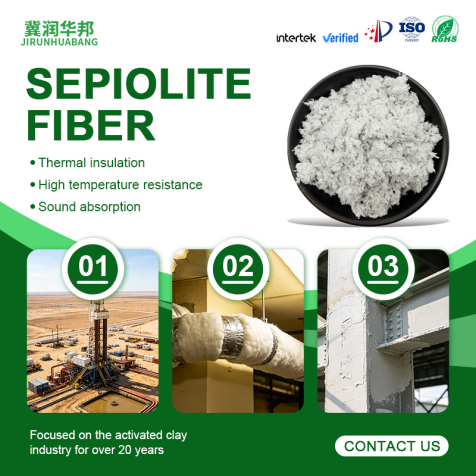
Beyond the core adsorption and purification performance, sepiolite fiber has five key industrial advantages: high temperature resistance, heat insulation and flame retardancy, salt and alkali resistance, thixotropic thickening, and reinforcement and crack resistance, adapting to various complex working conditions. In terms of high temperature resistance, its crystal structure remains complete and stable below 800℃ without cracking, shrinkage or pulverization, with a limit melting point of 1500–1700℃. It can be used for a long time in high-temperature working scenarios such as fire resistance, thermal insulation and high-temperature friction, far outperforming conventional inorganic fillers. In terms of chemical stability, it resists weak acid, weak alkali and high-salt corrosion, and will not flocculate, settle or fail in high-salt strata, industrial acid-base wastewater and corrosive fluid systems.
Its outstanding water-based thixotropy is particularly remarkable. When evenly dispersed in water-based systems, it forms a stable colloidal network structure with reversible thixotropic characteristics of “thickening at rest and thinning under stirring”. During the static storage of coatings, putty and water-based slurries, the system viscosity increases automatically, effectively preventing filler sedimentation, delamination and caking. During construction stirring, spraying and scraping, the viscosity decreases with shear force, ensuring smooth construction, strong wall adhesion and excellent leveling effect, greatly improving the construction quality and storage stability of terminal products. Meanwhile, the interlaced needle-like fibers build a three-dimensional supporting skeleton inside composite materials, significantly enhancing the tear resistance, impact resistance, crack resistance, wear resistance and weather resistance of products, realizing dual values of filling thickening and structural reinforcement.
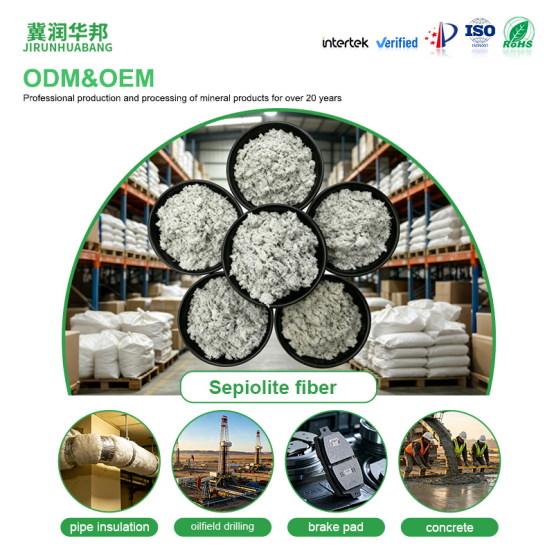
Relying on diversified excellent performances, sepiolite fiber covers the entire industrial chain and meets the high-end production needs of multiple industries. In the friction and sealing industry, it is the core filler for asbestos-free brake pads, clutch facings, mechanical sealing gaskets, flexible packings and industrial friction brake accessories. It effectively improves the wear resistance, heat resistance and impact resistance of products, reduces braking noise and thermal recession, replaces traditional asbestos fibers, and meets asbestos-free safety production standards. In the field of fireproof building materials, it is widely used in ultra-thin, thin and thick steel structure fireproof coatings, fire-resistant putty, fire-resistant thermal insulation boards and fire blocking materials, which can enhance coating adhesion and crack resistance, extend fire resistance limit, and prevent coating peeling and pulverization under high temperature.
In the field of rubber and plastic composite materials, as a modified filler added to rubber, plastic, PVC and composite materials, it can significantly improve the flame retardancy, aging resistance, tear strength and dimensional stability of materials, and extend the service life of rubber and plastic products. In environmental water treatment and waste gas treatment, it serves as a high-efficiency adsorbent for industrial wastewater decolorization, heavy metal ion adsorption, oil-water separation, aquaculture water purification and industrial waste gas deodorization and dust removal, which is green, pollution-free and recyclable. In petroleum, geothermal and mine drilling industries, it is a special high-end drilling mud additive. Relying on its salt-resistant thickening, cuttings carrying and wellbore stabilizing properties, it adapts to high-salt strata, deep wells and complex geological drilling conditions, avoiding wellbore collapse and mud failure. In addition, it is widely used in feed carriers, chemical catalyst carriers, brewing decolorization, thermal insulation slurries, daily chemical fillers and other segmented fields with strong versatility.
As a direct manufacturer, we supply full-series sepiolite fiber products including long and short fibers, ultra-fine powder and modified activated fibers. We can customize and adjust fiber length, purity, whiteness, fineness and surface modification technology according to customers’ production formulas, application scenarios and process requirements, perfectly adapting to the production standards of different industries. Our factory has complete production lines and quality inspection systems, with full-process control from raw ore screening, purification and defibering, drying and grading to packaging and delivery. All batches have stable indicators, no impurities and excellent dispersibility. We support customized packaging of 25kg bags and jumbo bags, meeting the needs of small-batch sample testing and large-batch foreign trade orders. We accept various international trade terms such as FOB, CIF and CFR with stable supply and controllable delivery time. Global factories, traders and purchasing customers are welcome to consult for samples and negotiate long-term strategic cooperation.
 Hot News
2026-03-17
2025-12-08
2025-12-06
2025-12-02

Runhuabang supplies non-metallic minerals, including iron oxide pigments, silica powder, kaolin, diatomite and zeolite and so on, with custom solutions worldwide.
H2-811, Poly International Building, Shifang Road, Chang'an District, Shijiazhuang, Hebei Province
Copyright © Hebei Runhuabang New Material Technology Co., Ltd All Rights Reserved Privacy Policy
 EN